Framing
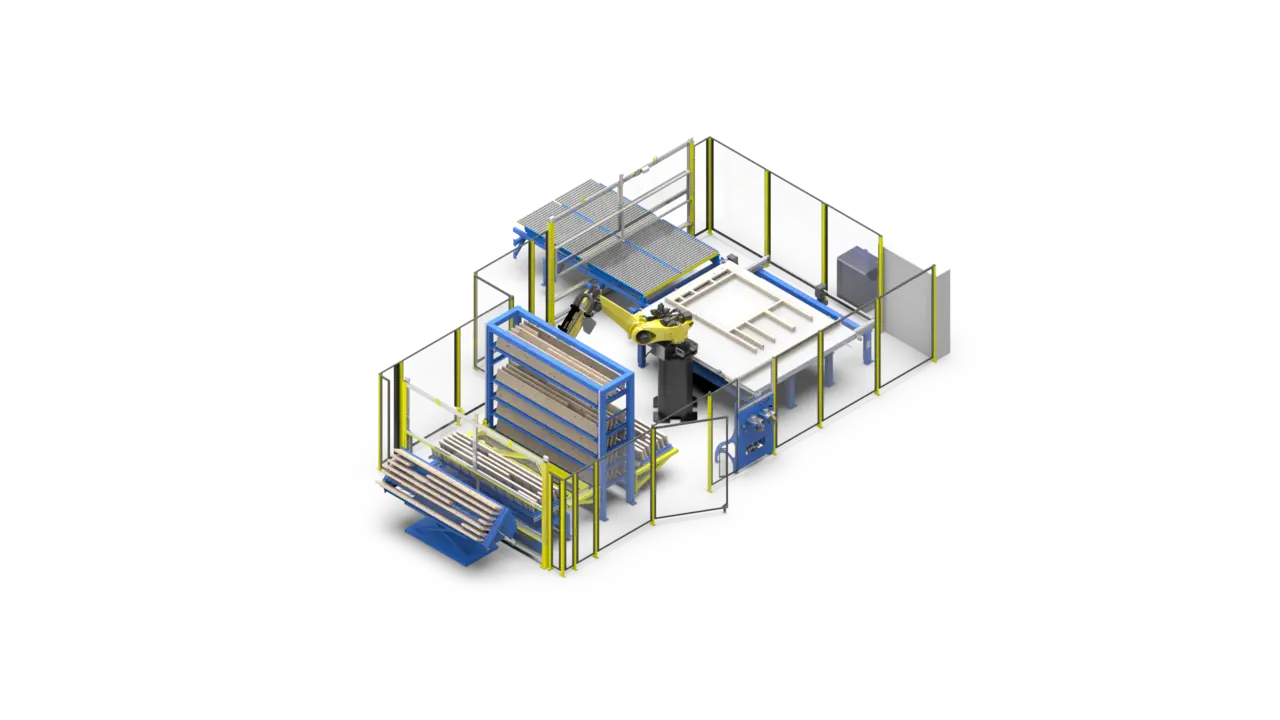
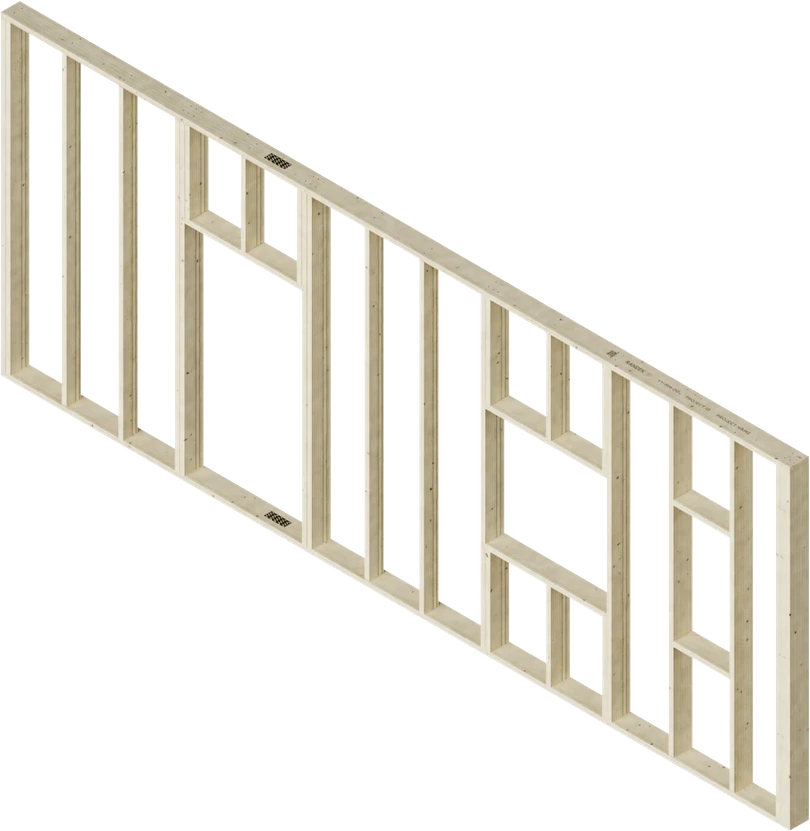
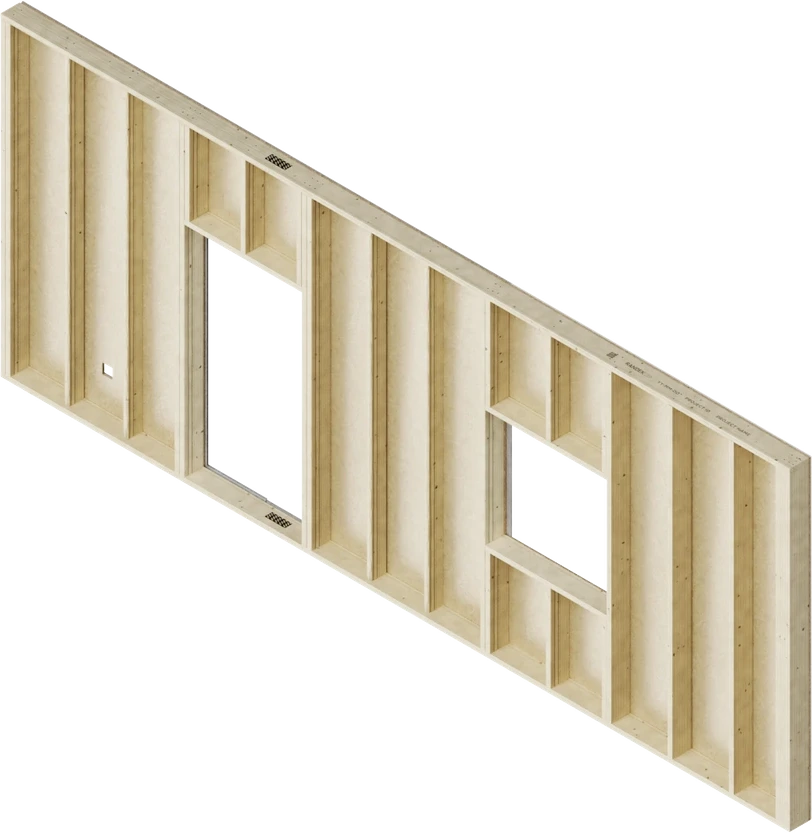
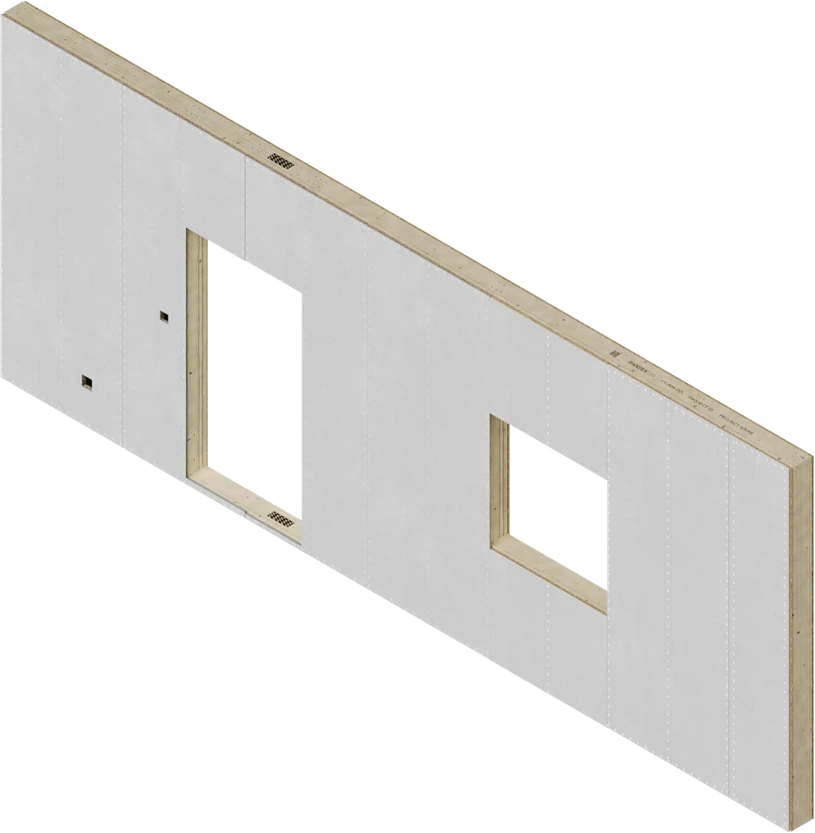
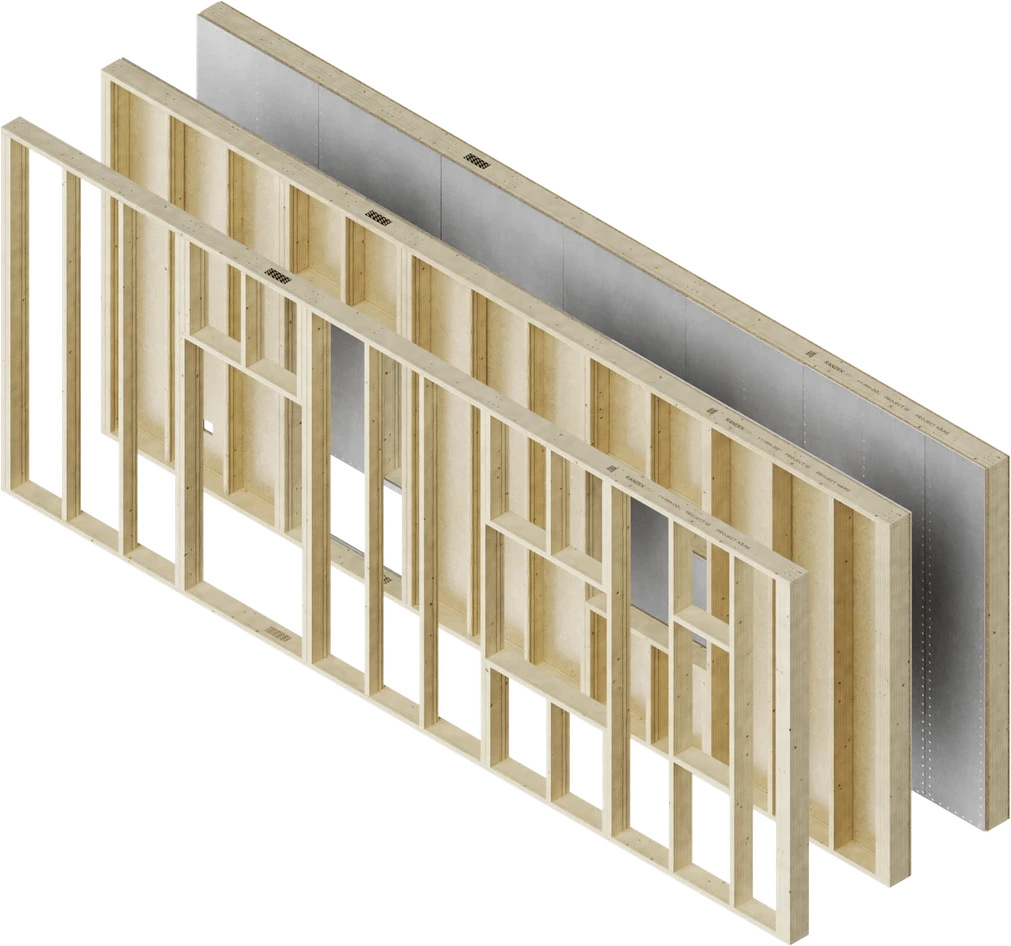
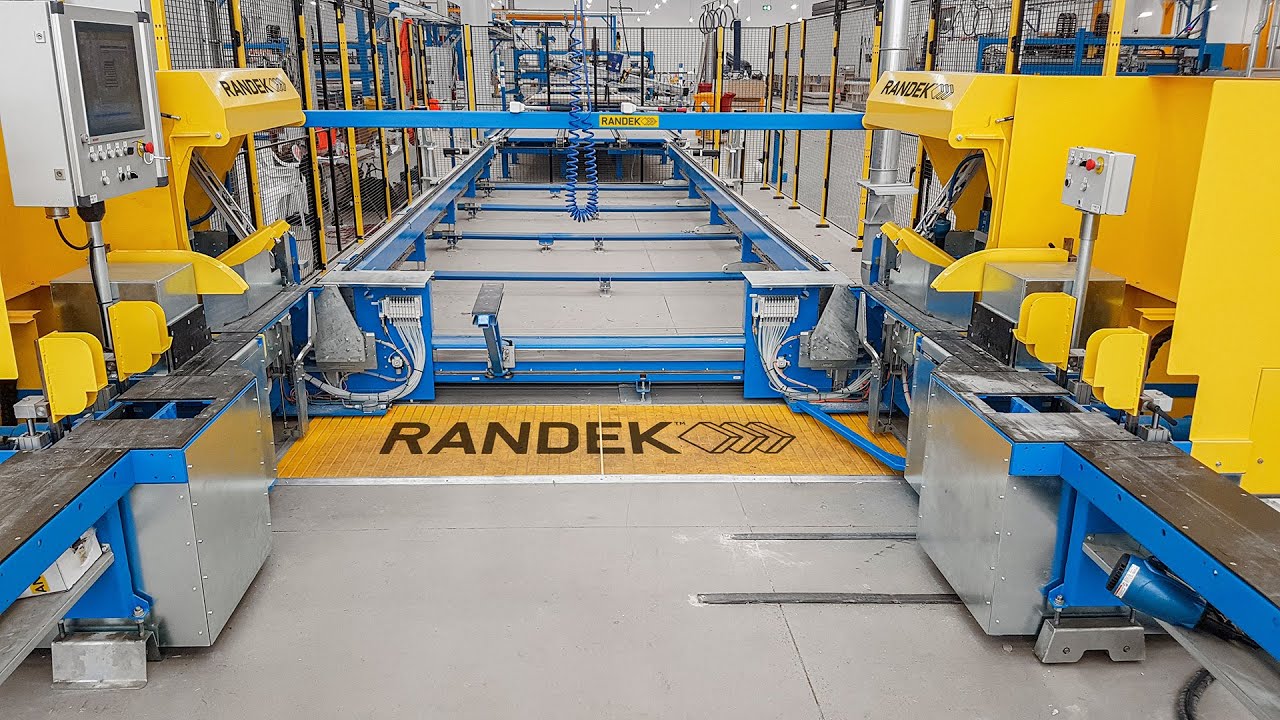
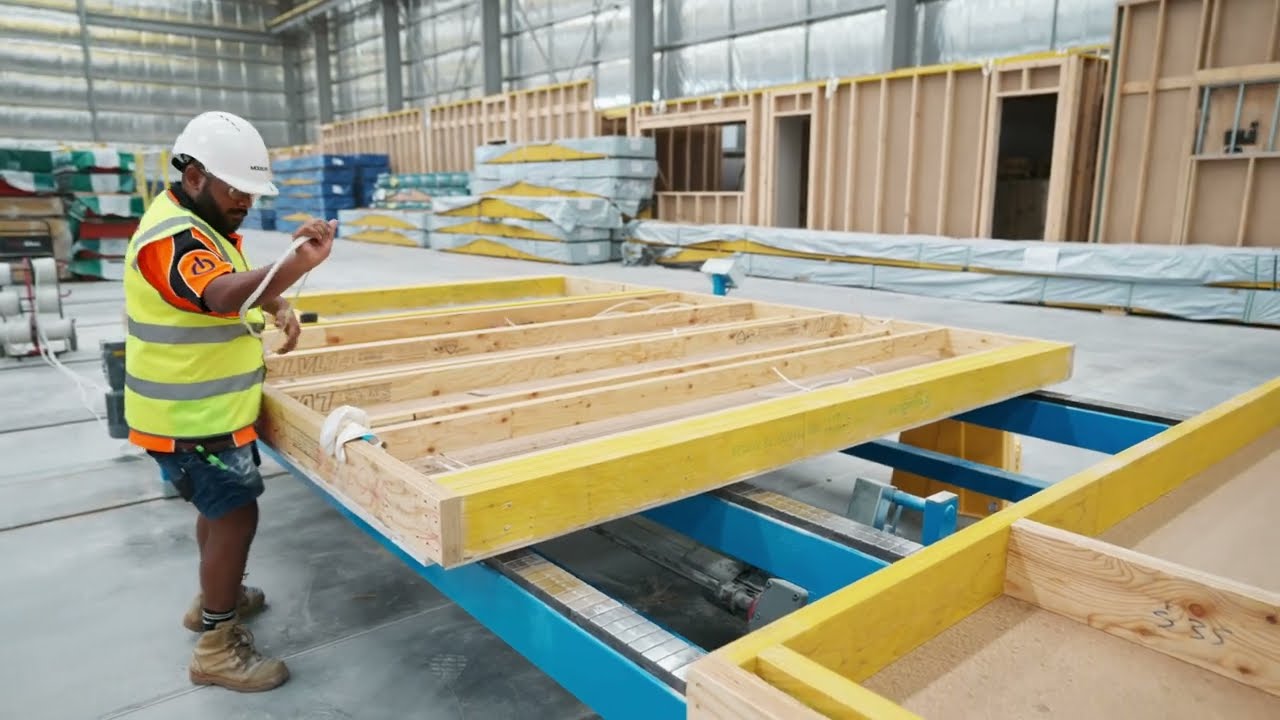
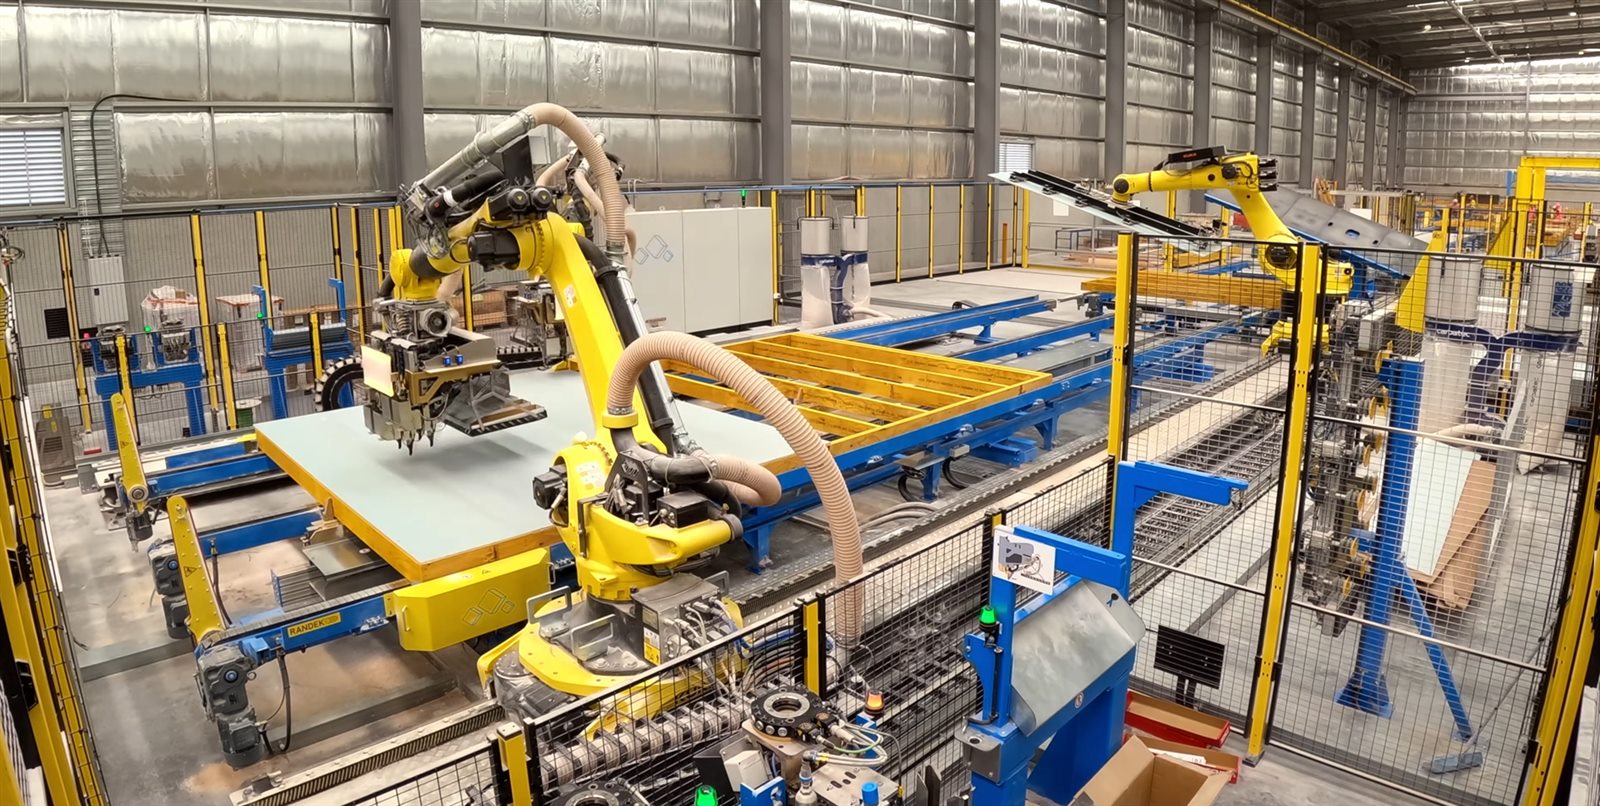
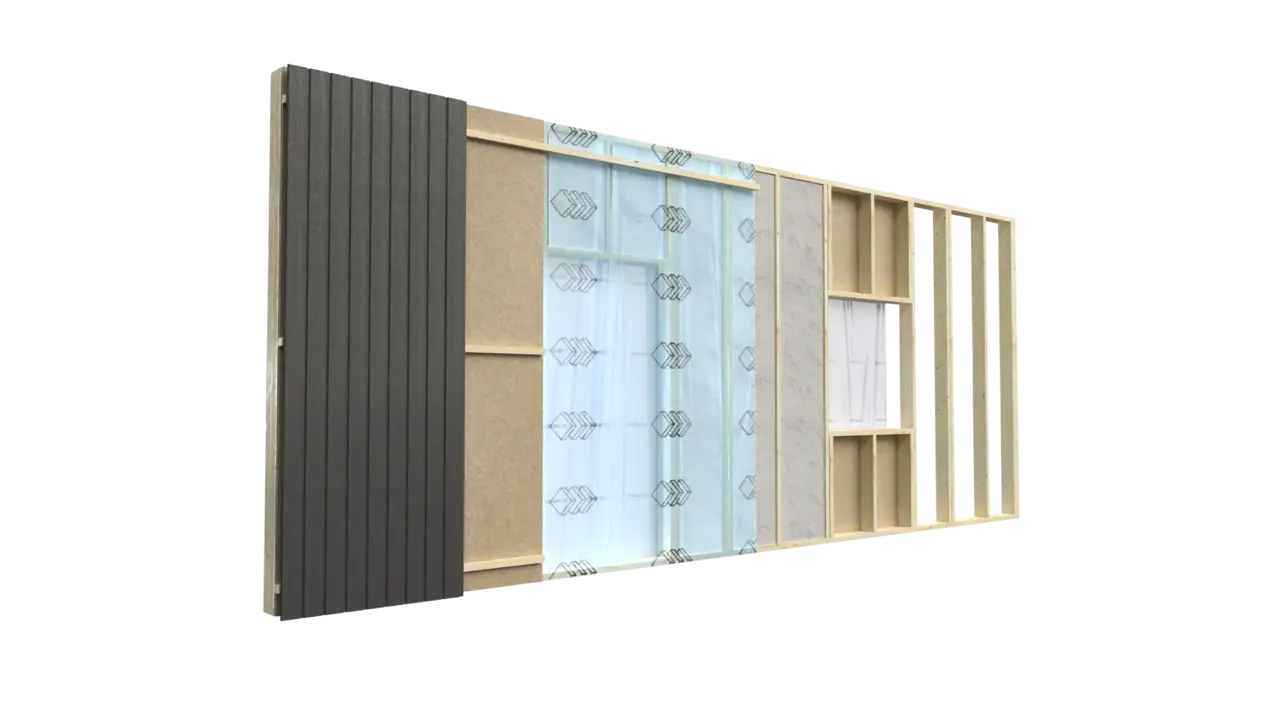
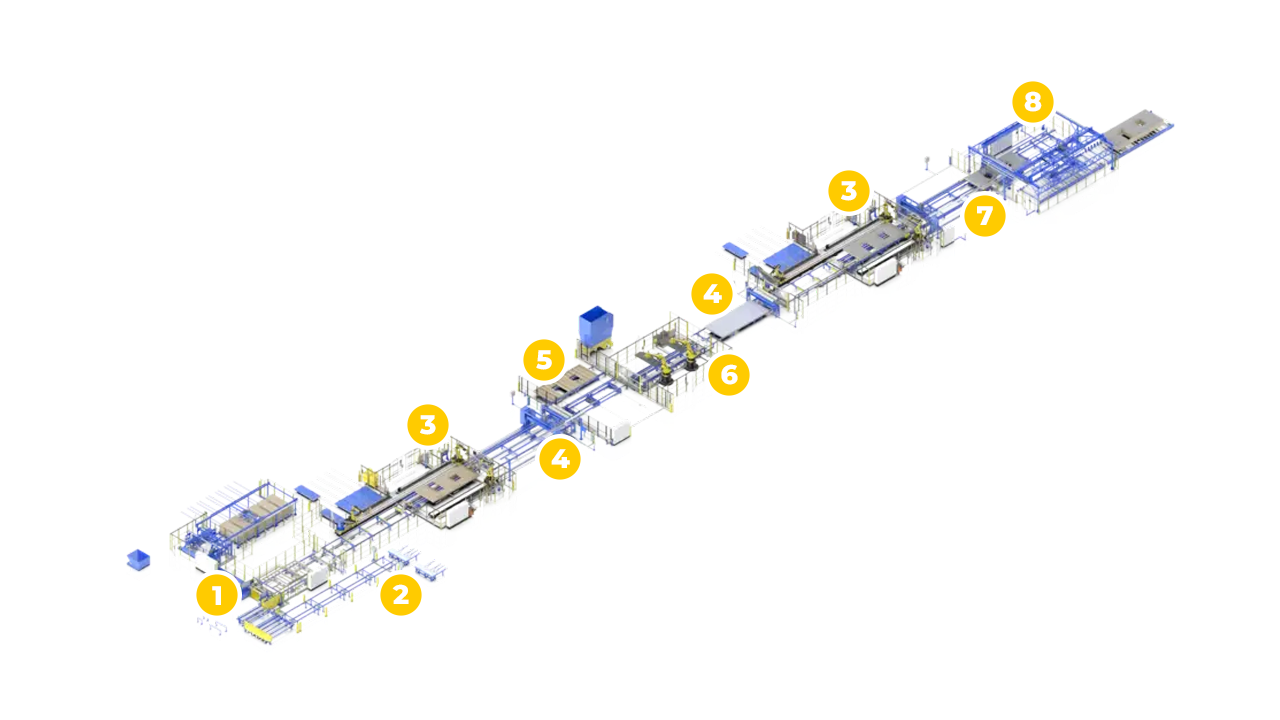
The start of the line, where the timber frame of bottom plate, top plate, studs and sub-elements is assembled and nailed square before it moves on.
The same station slot, framing in light gauge steel instead of timber. From the frame on, the element runs the same AutoWall stations.
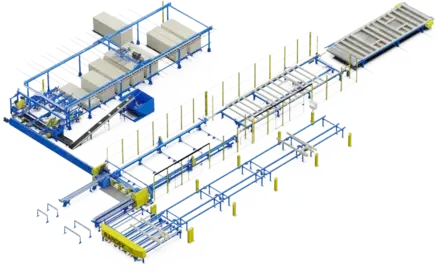
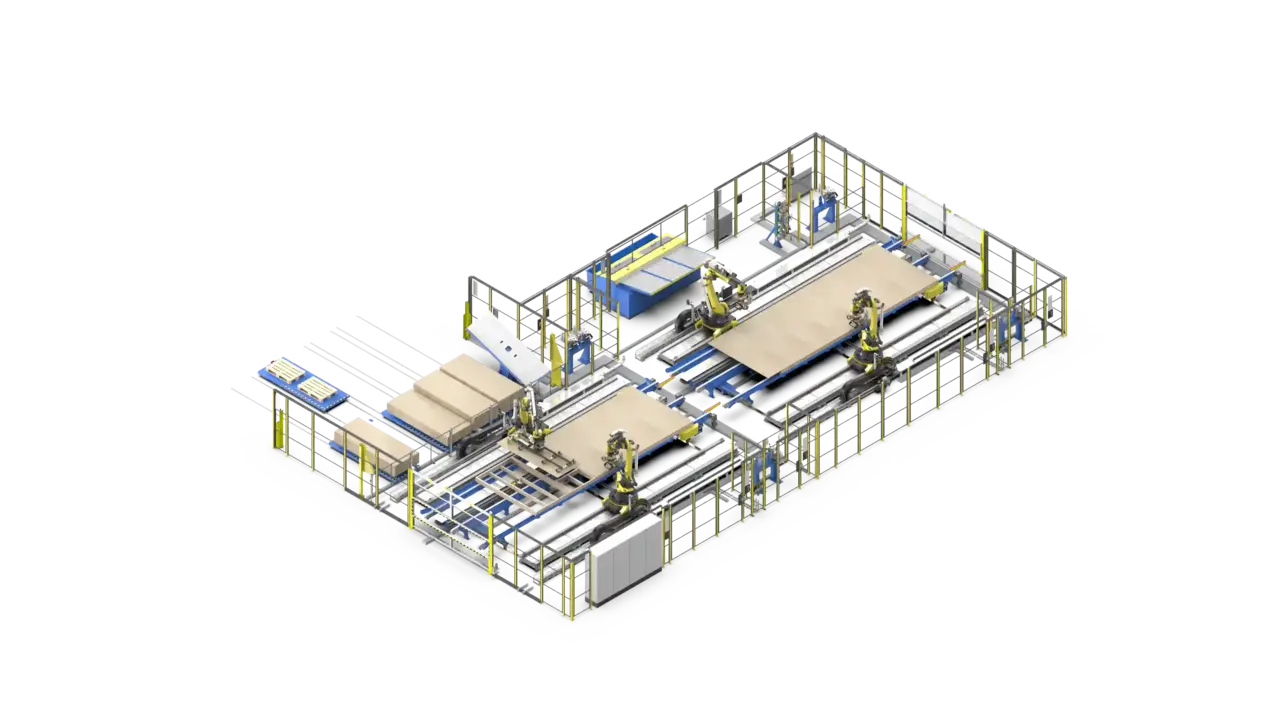
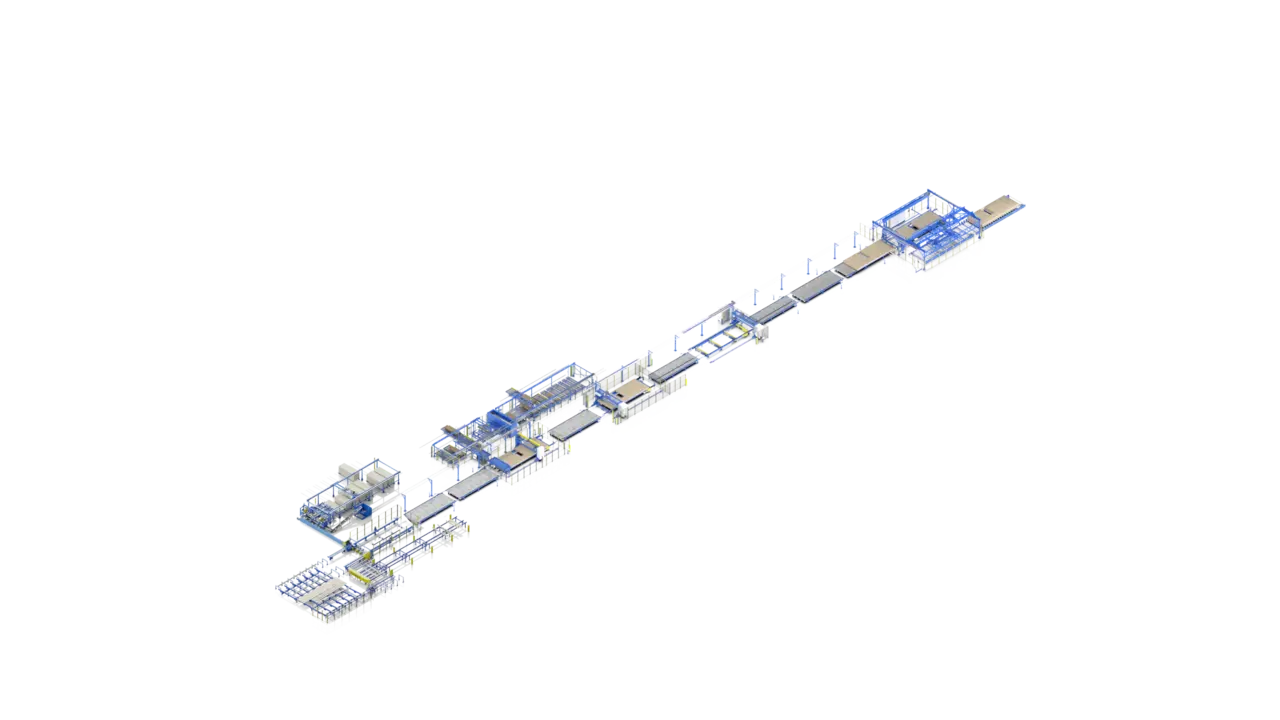
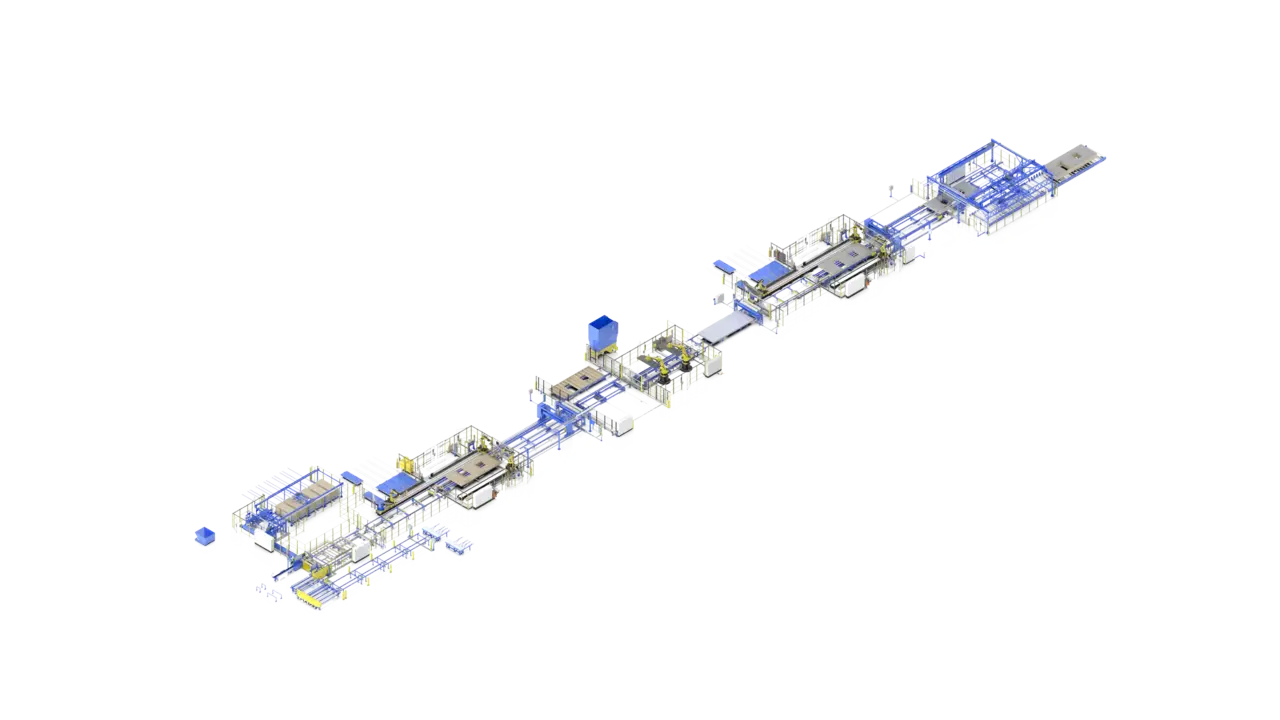
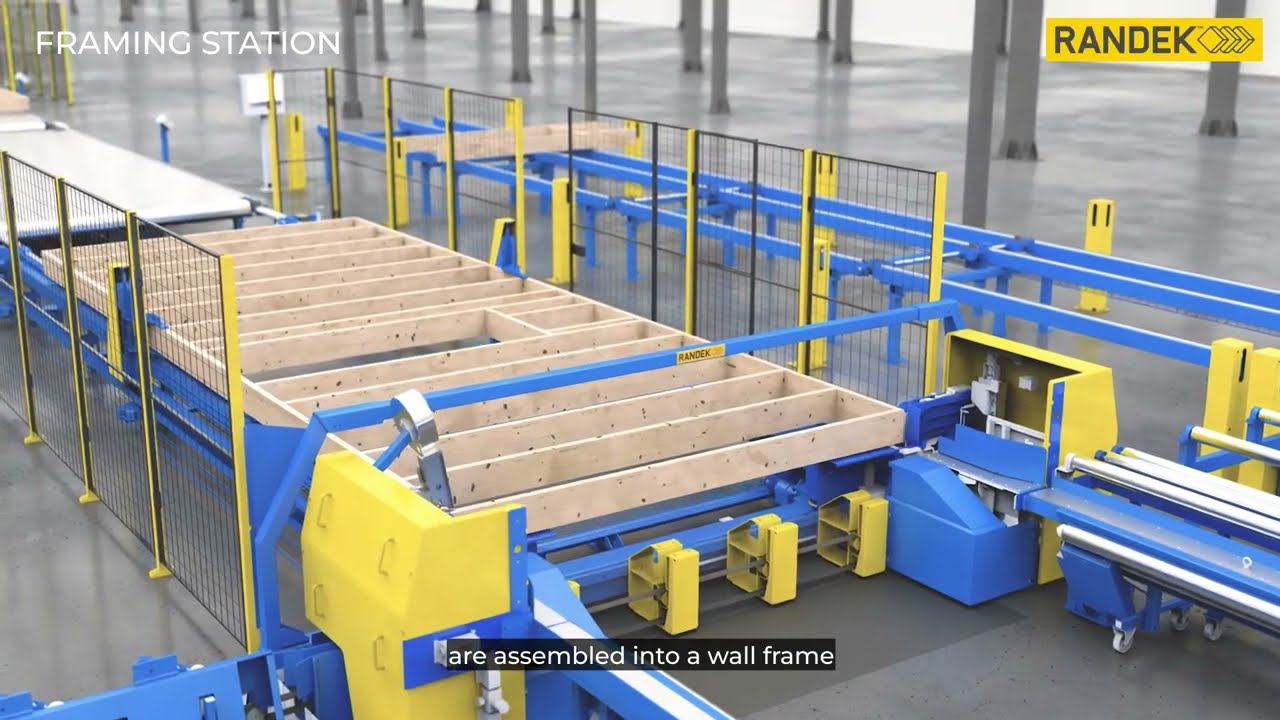
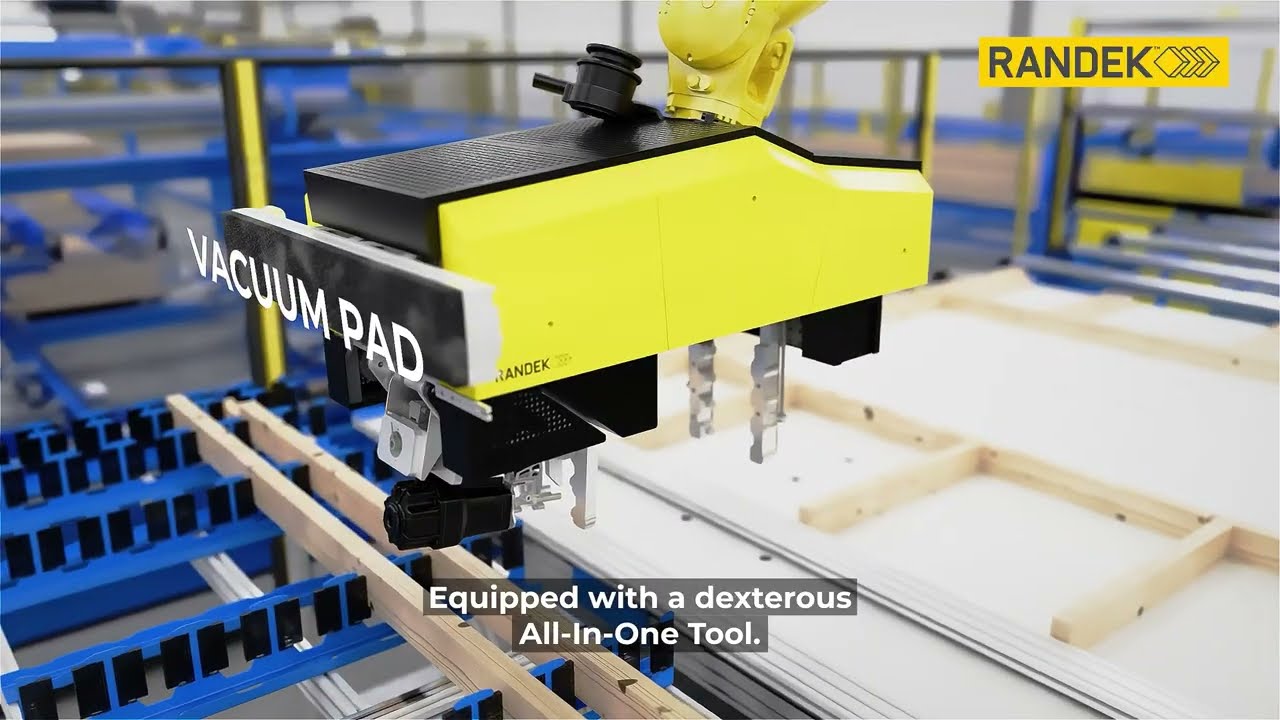
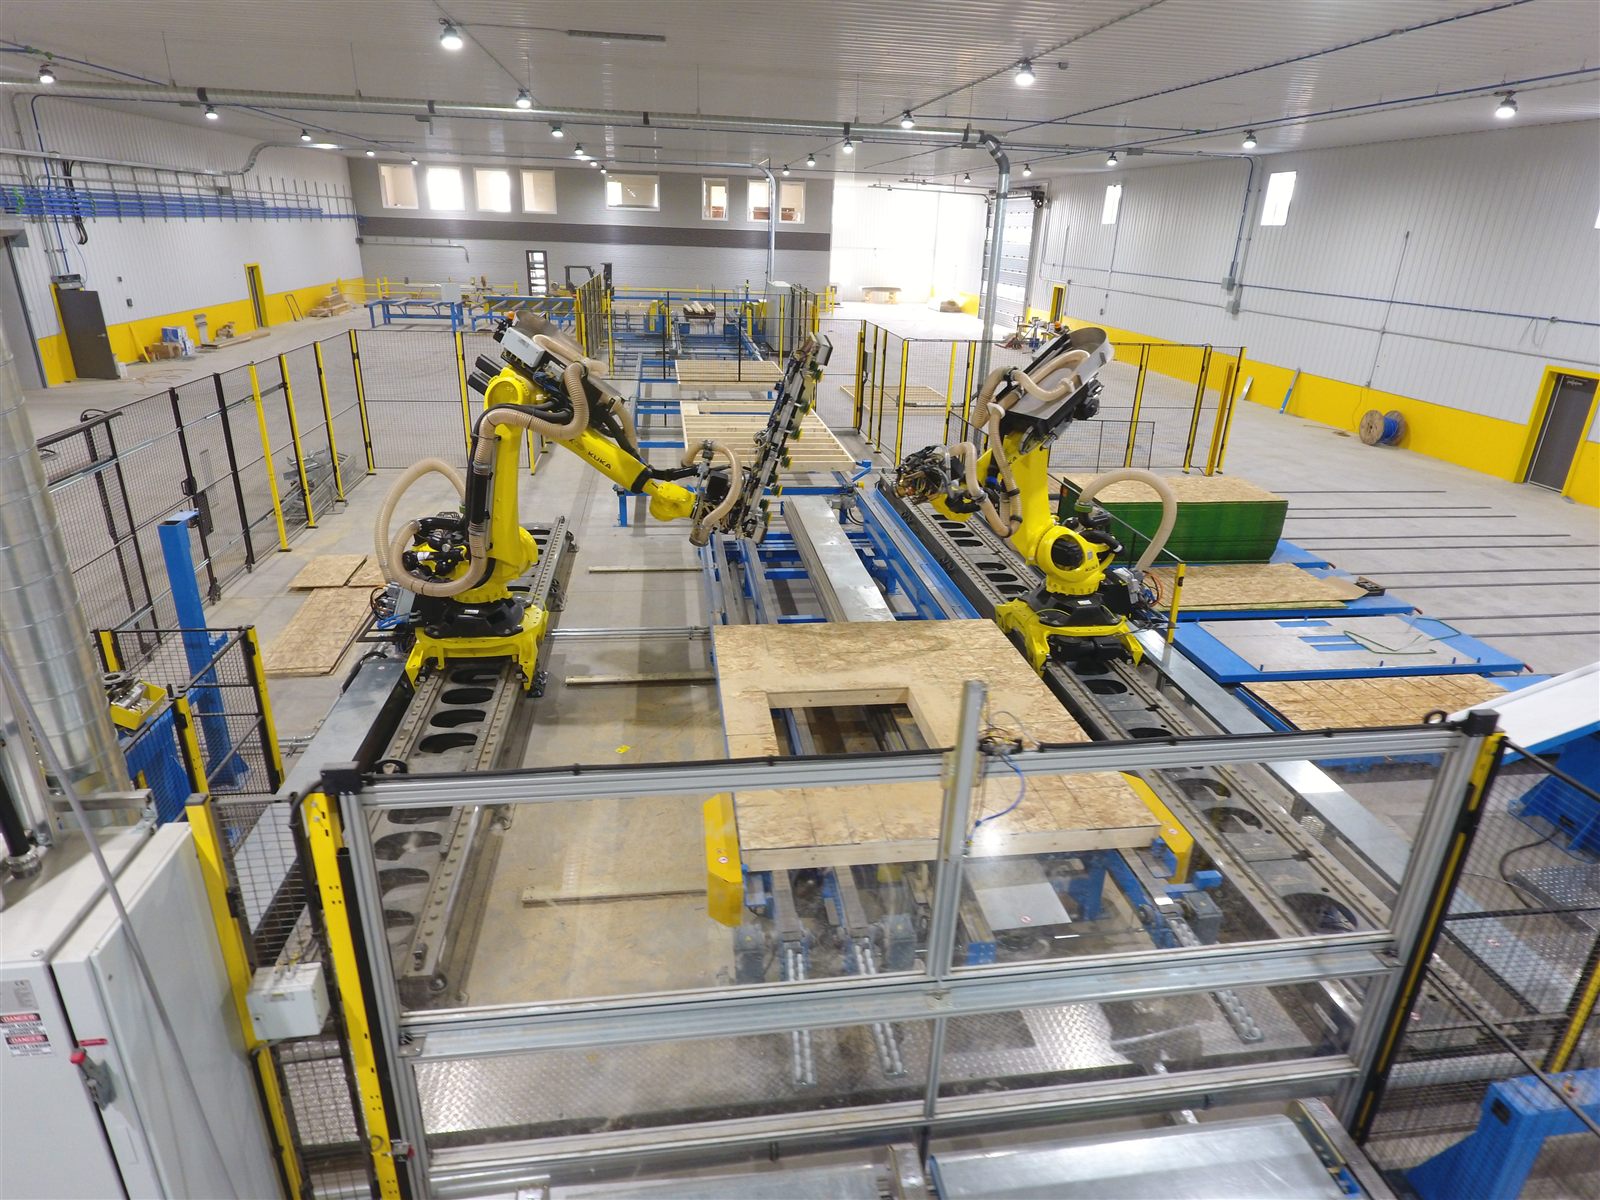
The automated framing station positions and nails studs, plates and noggins from the CDT file, and squares the frame before it leaves.
Feeds studs from packages straight off the trolley.
Feeds bottom and top plates into the station.
Cuts noggins to the actual distance between the studs, so stud-thickness deviation does not carry into the element.
Lasers inspect each stud, flip it so the crown faces the same way, and reject studs outside the bending range.
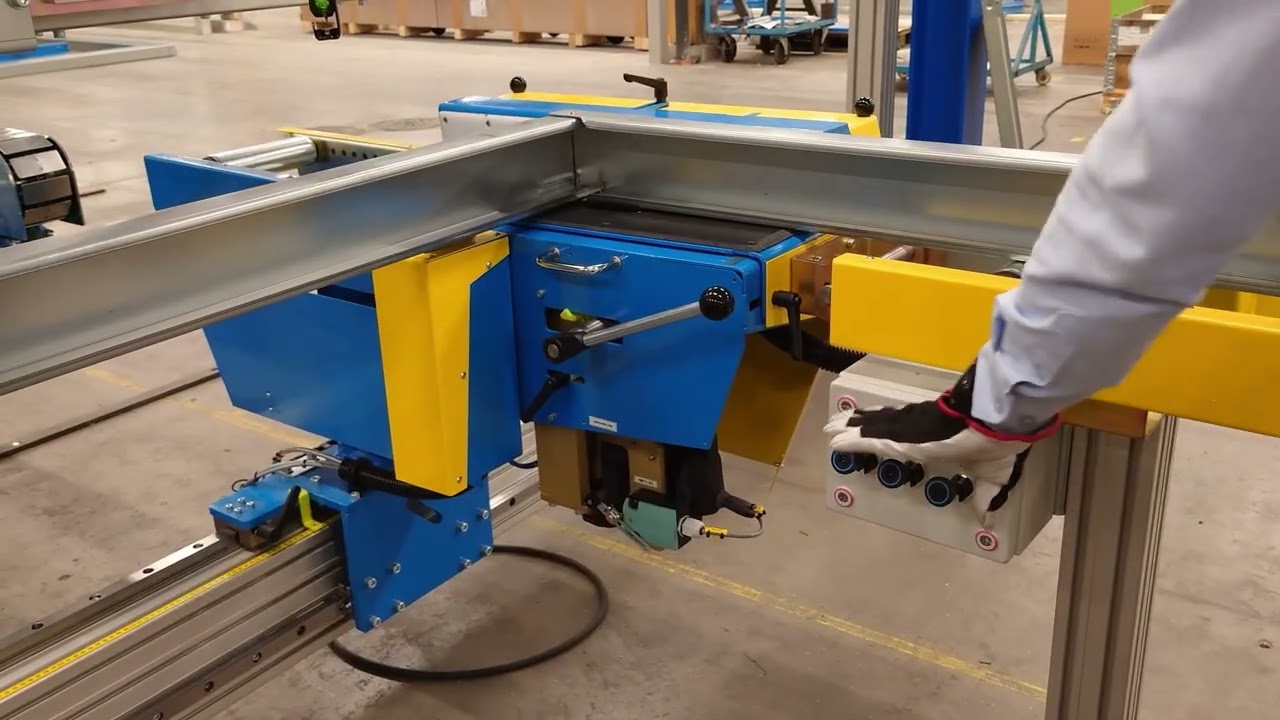
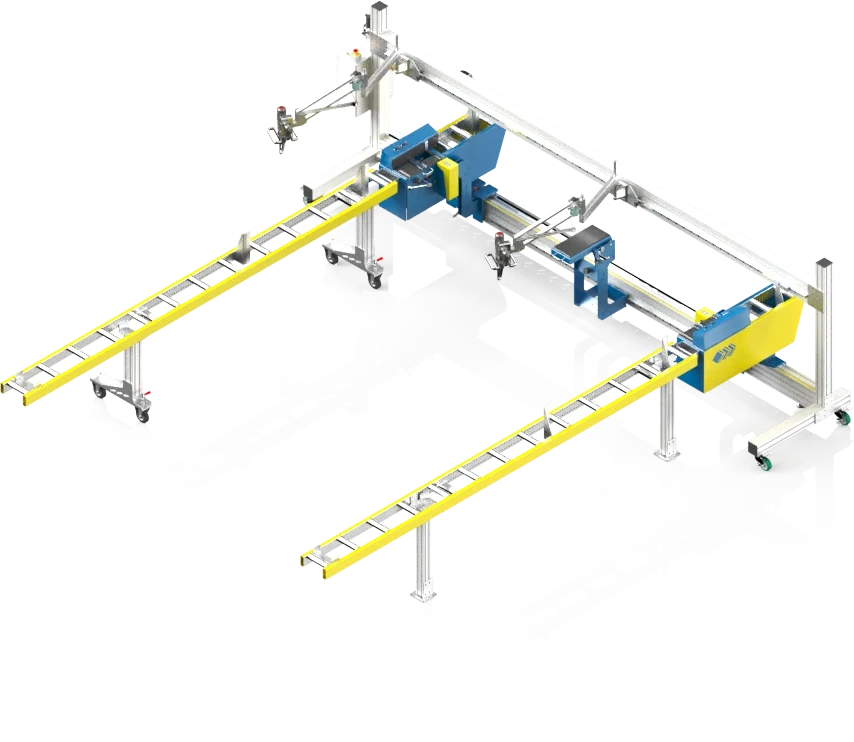
Upper and bottom screwdrivers fasten the studs into the top and bottom plates in one station; plate and stud stops set the position and the operator builds each frame by hand.
See it →Driven from the CAD/CAM file: the frame is fed forward automatically in steps, and up to six automatic screwing units, three above and three below, drive the screws from both sides.
See it →